Understanding Standardised Chemical Pumps

Understanding Standardised Chemical Pumps

A standardised chemical pump plays a crucial role in modern industrial applications where consistent performance, safety, and durability are essential. These pumps are engineered according to international standards, ensuring high interchangeability and reliability for handling a variety of corrosive and hazardous chemicals. They are widely used in industries such as chemical processing, pharmaceuticals, petrochemicals, and water treatment.

Efficiency and Chemical Compatibility

One of the most important advantages of a standardised chemical pump is its ability to handle aggressive media. Whether it’s an Acid circulating pump for sulfuric acid or an hcl transfer pump for hydrochloric acid, these pumps provide excellent corrosion resistance and stable flow performance. The materials used—such as PTFE, PVDF, or UHMW-PE—help ensure safe chemical transfer even under demanding conditions.

Application in Sodium Hypochlorite Systems

For facilities managing disinfectants or oxidizing chemicals, the Sodium hypochlorite centrifugal pump is a vital component. It is designed to withstand the oxidative stress and corrosive nature of sodium hypochlorite, ensuring long-lasting operation and minimizing maintenance downtime. When integrated with standardized designs, these pumps provide greater operational safety and reduced leakage risks.

Design and Performance Advantages

Standardised chemical pumps offer high efficiency, modular construction, and easy replacement of parts. Their optimized hydraulic design reduces energy consumption while maintaining high flow rates and consistent pressure. This makes them ideal for continuous industrial use where both reliability and cost-efficiency are critical.

Safety and Maintenance

These pumps are equipped with advanced sealing technologies that prevent leakage of toxic or volatile chemicals. The standardized structure allows for easier maintenance and part interchangeability, minimizing downtime during repairs or inspections.

Environmental and Operational Benefits

Standardised chemical pumps contribute to sustainable operations by reducing waste, leakage, and energy usage. Their robust design supports long-term use in harsh environments, from chemical plants to wastewater treatment facilities.

UHMW-PE Centrifugal Pump – The Ideal Choice

At the core of corrosion resistance and durability lies the UHMW-PE centrifugal pump. Known for its superior wear and chemical resistance, UHMW-PE material ensures stability even when transferring strong acids, alkalis, and solvents. It’s perfectly suited for applications in chemical manufacturing, electroplating, pickling, and water treatment industries.

Why Choose RISTER PUMPS

RISTER PUMPS is a trusted manufacturer recognized for precision engineering, material innovation, and excellent customer service. With extensive experience in designing standardised and customized chemical pumps, RISTER provides solutions that combine efficiency, safety, and longevity. Their technical expertise and responsive after-sales service make them a preferred partner for global industries handling aggressive and corrosive fluids.

In every standardised chemical pump solution, RISTER PUMPS delivers not just reliable equipment but also long-term value through professional support, customization, and continuous innovation.
Unlocking Efficiency with Self-Priming Pumps in Chemical Applications

Unlocking Efficiency with Self-Priming Pumps in Chemical Applications


In demanding chemical processing environments, equipment reliability and efficiency are non-negotiable. Among the most versatile and dependable tools in this field is the self-priming pump. Unlike traditional centrifugal pumps, a self-priming pump can evacuate air from the suction line and prime itself without needing manual intervention or additional vacuum systems—making it a preferred choice across various industries.


A self priming chemical transfer pump is particularly valuable in handling aggressive or hazardous liquids. Its ability to manage both fluids and air mixtures without losing pumping capacity makes it ideal for chemical unloading, transfer, and circulation applications. Whether in offloading tanks or circulating chemicals through treatment systems, these pumps offer both safety and performance.


The self priming chemical pump is engineered to resist corrosion, often constructed with materials like stainless steel, polypropylene, or fluoropolymers. This ensures long-term durability when working with acids, alkalis, or solvents. Additionally, its easy maintenance and minimal operational oversight reduce downtime, making it a smart investment for facilities seeking efficiency and cost control.


Choosing the right self priming pump manufacturer is crucial. Beyond technical specifications, manufacturers must offer proven reliability, custom options, and expert guidance tailored to your application. An experienced manufacturer can also help integrate self-priming pumps into complex systems with minimal modification or disruption.


RISTER stands out as a trusted name in the field of self priming pumps. With decades of engineering experience and a focus on chemical compatibility, RISTER provides high-performance pumps designed for safety, efficiency, and longevity. Their self-priming chemical pumps are precision-built to handle corrosive fluids with ease and are backed by responsive technical support and tailored solutions. For businesses seeking a reliable partner in fluid handling, RISTER offers unmatched value and expertise.


Why PTFE Lined Piping Is the Ideal Solution for Corrosive Fluid Transport

Why PTFE Lined Piping Is the Ideal Solution for Corrosive Fluid Transport

In industries that deal with aggressive chemicals and high-purity processes, the choice of piping material is critical. PTFE lined piping offers outstanding chemical resistance, making it a top solution for safely transporting corrosive media. Unlike conventional metal or rubber lined pipe options, PTFE lining provides superior durability, non-stick performance, and resistance to almost all industrial acids, bases, and solvents.

Lined Pipe: The Smart Investment for Long-Term Reliability

A lined pipe combines the strength of metal with the chemical resistance of internal liners such as PTFE or PFA. While rubber linings are suitable for some mildly corrosive applications, they often degrade over time when exposed to highly aggressive chemicals or elevated temperatures. PTFE, on the other hand, is virtually inert and operates efficiently across a wide temperature range, making it ideal for chemical, pharmaceutical, and semiconductor industries.

The Role of PFA Lined Tees in System Integration

For complex piping networks, fittings like the PFA lined tee are essential. These components allow for multi-directional flow and system flexibility without compromising chemical resistance. PFA, a close cousin to PTFE, offers excellent clarity and mechanical strength, making it ideal for high-purity environments. Combined with PTFE-lined pipes, PFA lined tees ensure that every part of the fluid path is protected from corrosion and contamination.

RISTER+PIPE: Engineered Excellence in Lined Piping Solutions

When it comes to quality and reliability, RISTER+PIPE stands out in the industry. As a trusted supplier of PTFE lined piping, rubber lined pipe, and custom PFA-lined components, RISTER delivers superior craftsmanship and technical expertise. All products are manufactured to meet international standards, ensuring safety, longevity, and process compatibility.

In addition to top-tier product quality, RISTER+PIPE provides tailored solutions, fast delivery, and expert support. Whether you're upgrading an existing system or building a new process line, RISTER ensures that your lined piping system performs flawlessly—making them the preferred partner for industries where chemical resistance and safety are non-negotiable.

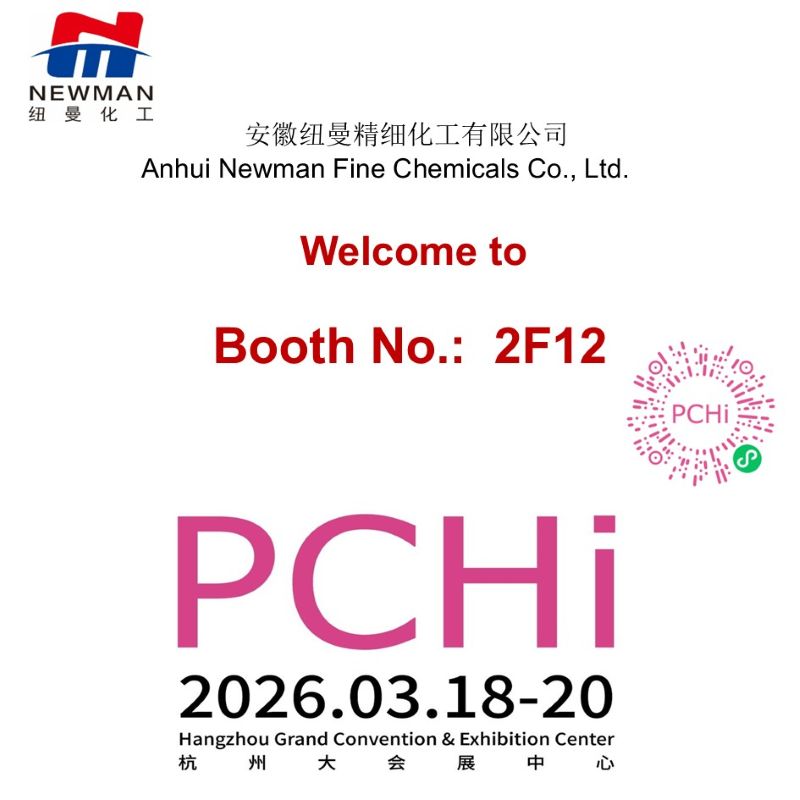
Welcome our booth 2F12 PCHi 18-20.March 2026, Hangzhou, China

Personal care and home care ingredients (PCHi2026) will be held  at the Hangzhou Convention and Exhibition Center from March 18th to 20th, 2026. As an important event in the global personal care and household care products raw materials sector, this exhibition brings together 800+ exhibitors from around the world and 50,000+ industry professionals. Newman Chemicals will showcase its full range of products and customized solutions and will engage with global industry partners to discuss technological innovation and explore new development chapters.


Against the backdrop of accelerated domestic substitution and global supply chain restructuring, Chinese cosmetics raw material enterprises are experiencing unprecedented development opportunities. Newman Chemicals' participation in PCHI 2026 is not only a concentrated display of the innovation capabilities of local enterprises, but also demonstrates its determination to deeply integrate into the global industrial ecosystem and promote collaborative innovation in the industry.


PCHi 2026 Newman chemicals carbomer


We have been launching and improving our traditional carbomer 960,970,996, 990 etc., improve carbomer 20,21,10, and 30. Especially, we launched polymeric emulsifier  NM-Carbomer TR series, NM-Carbomer TR-1, TR-2 and TR-3 ,are versatile, non-ethoxylated polymer designed to create stable and mild oil-in-water emulsions at low use levels. Not only thickening ,suspending ability ,but also good emulsifying, and they are  great choice for use in many skin care formulations, providing emulsion stability, smooth texture, and a pleasant fresh sensory for emulsions.


At the same time, the liquid carbomer NM-Carbomer SF-1, NM-Carbomer Aqua10 and NM-Carbomer Aqua 20 are also introduced, which are easy to use liquid forms and have good synergic thickening effect with surfactants, micelles and hydrophobic raw materials due to special chemical structure. Excellent salt resistance. We also specially launched the NM-Carbomer Aqua 25, INCI name: Acrylates/ Steareth-20 Methacrylate Crosspolymer, NM-Carbomer Aqua 25 is an anionic hydrophobically modified alkali-soluble acrylic polymer emulsion (HASE) with unusually high aqueous thickening and stabilizing efficiency. Specifically imparting efficient thickening properties for amino acid surfactant systems, and has excellent clarity gels , which can be extensively applied for formulations containing high levels of surfactant.


Our heath care and Oral care grade carbomer are focused on, such as NM-Carbomer 934P as a thickener and co-binder for Aqueous toothpaste formulations , NM-Carbomer 974P as now preferred thickeners for anhydrous toothpaste formulations, and NM-Carbomer 971P for mouth rinses.


At the same time, we continue to launch film forming, thickening and lubrication polyvinylpyrrolidone homopolymer such as PVP K30, K90, K17, K25, and PVP/VA copolymer such as PVP/VA64, PVP/VA73 and other series of products.


Cherishing to see you at our booth 2F12. We are looking forward to sharing  our innovative achievements and discussing the future of personal care and home care fields.


What is the antioxidant effect of ferrite magnets?(1)

Contact more customers, there will always be a lot of questions, such as a user asked, ferrite magnet can be saved for how long? Does oxidation of ferrite affect its properties?

Today I will reply to these two questions.


Ferrite, also known as permanent magnet ferrite, chemically known as ferric oxide, is already an oxide of iron, and it is difficult to be oxidized again. For the magnetic ring, its characteristics are long-term, there will be no deterioration, but put for a long time, there will be residue on the surface - some powder, this is a normal phenomenon, does not hinder its characteristics.


As we all know, ferrite magnet is made of a variety of magnetic materials, so put for a long time, the magnet will appear powder, which is what we say in the industry oxidation, but this does not affect its magnetic properties and impedance characteristics. The magnet will also be easy to oxidize when it encounters moisture, especially in wet weather. If the magnetic ring of the packaging is not sealed well and the moisture runs into the carton, it will also lead to oxidation of the magnetic ring.


Many people will ask, the magnet in production is not through water to clean the surface? How can also be afraid of water, of course, the magnetic ring is through the water to wash off the dirty surface, but after cleaning, the magnet to enter the oven to dry water, so just made of the magnet, not oxidation, and just washed out of the magnetic ring appearance, shiny!


Recommendation for Magnet Selection

Recommendation for Magnet Selection


1. Project Assessment

Begin by clarifying the application requirements:

 Application Scenario: Identify the purpose (e.g., industrial machinery, consumer electronics, medical devices).

 Force Requirements: Determine the necessary magnetic strength (e.g., high-precision motors require strong magnets like NdFeB)

 Temperature Range: Select materials based on operating temperatures. For example:

 N-series NdFeB: Suitable for 80°C.

 H/SH/UH/AH-series NdFeB: Higher temperature resistance (up to 230°C)

 Environmental Conditions: Consider corrosion risks (e.g., NdFeB requires nickel or epoxy coatings for humidity resistance)

2. Magnet Material Selection

Compare key magnetic materials (weakest to strongest):

1. Rubber Magnets: Low cost, flexible (ideal for signage, calendars, crafts)

2. Ferrite Magnets: Affordable, widely used in motors and speakers

3. AlNiCo Magnets: High-temperature tolerance (~500°C), stainless appearance (suitable for instruments)

4. Samarium Cobalt (SmCo): Heat-resistant (150300°C), brittle but durable in harsh environments

5. Neodymium (NdFeB): Highest magnetic strength, cost-effective, but prone to oxidation (requires coatings)

3. Supplier Communication Strategy

When contacting clients (e.g., manufacturers or distributors):

 Key Questions to Ask:

 Do you provide customized shapes (e.g., discs, rings, blocks)?

 What certifications do your products hold (e.g., ISO, RoHS)?

 Can you share test reports for magnetic performance and durability?

 Sample Request: Request samples to verify quality and compatibility with your application.

 Cost and Lead Time: Compare pricing and delivery timelines across suppliers.


How to Design a Perfect Outdoor Living Space with Goodwin Furniture's Sofa and Dining Sets

Designing the perfect outdoor living space involves creating a harmonious blend of comfort, style, and functionality. Goodwin Furniture offers an exquisite range of sofas and dining sets that can transform any patio or backyard into a serene oasis.

Start by selecting a suitable area in your outdoor space, ensuring it is well-lit and has a view. Next, choose a Goodwin sofa set that complements your aesthetic—whether modern, rustic, or coastal. Opt for weather-resistant fabrics and finishes to ensure durability against the elements. Arrange the sofas to create an inviting seating area, perfect for relaxation or entertaining guests.


Incorporate a dining set from Goodwin Furniture to enhance your outdoor gatherings. A sturdy table paired with comfortable chairs invites alfresco dining experiences. Consider adding an umbrella or pergola for shade, making the space usable throughout the day.


To complete the look, accessorize with outdoor cushions, throw blankets, and decorative lighting. Greenery, such as potted plants or climbing vines, adds life and color. With Goodwin Furniture's stylish pieces, your outdoor living space can become a tranquil retreat, ideal for both leisure and socializing.


Quality Outdoor Furniture  will bring durable beauty over time and safety for users. With a variety of models, designs, materials and different prices of outdoor furniture products,Goodwin outdoor furniture provide you with pieces that meet your expectations for quality, comfort, and design , with additional pieces, colors, and fabric options available by special order. Please inquire for lead times on orders.

Elevate Your Tastings with Single-Wall Mini Paper Cups

When it comes to olive oil tastings, espresso samples, or any small-volume beverage service, presentation matters — and so does sustainability.  The single-wall mini paper cup offers a sleek, minimalistic option that doesn’t distract from the flavor experience.   Lightweight and simple, these cups provide an elegant, eco-friendly alternative to heavier or coated cups, preserving the true aroma and character of your liquid.


Designed for Olive Oil Tasting, Coffee Sampling & More

Our single wall 2.5 oz, 3 oz, 3.5 oz, 4 oz olive oil tasting / mini coffee paper cup is engineered for precision and practicality.   The uncoated, single-wall construction is ideal for short-duration sampling: it’s disposable and yet fully functional for delicate tastings.   Whether you’re offering extra virgin olive oil flights or espresso shots, this cup keeps things simple and clean.   The compact size is perfect for tastings, sampling events, specialty cafés, or promotions.


Perfect for Tastings, Trade Shows, and Cafés

If your business hosts tasting events, food fairs, or boutique café offerings, these mini paper cups are an excellent choice.   Their form factor is ideal for pour-over presentations or oil flavor profiles without overwhelming customers with large volumes.   Because they’re disposable, cleanup is easy — and because they’re paper, they make a more sustainable impression than plastic.   Guests can focus on flavor, you can focus on service, and waste is kept to a minimum.


biosettings: Where Sustainability Meets Service

At biosettings, we’re committed to delivering eco-friendly products that don’t compromise on purpose or performance.   Our mini single-wall paper cups reflect that philosophy: simple, functional, and planet-friendly.   Choosing biosettings means choosing a brand that cares about every detail — from your tasting experience to environmental impact.

Frequently asked questions about PE coated paper rolls

PE coated paper roll refers to a roll of paper that has been coated with a layer of polyethylene (PE) on one or both sides. This coating provides the paper with enhanced durability, moisture resistance, and heat-sealing properties. It is commonly used in various industries for packaging, labeling, and food service applications.

Here are ten frequently asked questions about PE coated paper rolls:

1. What is the purpose of the polyethylene coating on the paper roll?
The polyethylene coating provides moisture resistance, durability, and heat-sealing capabilities to the paper.

2.What industries commonly use PE coated paper rolls?
PE coated paper rolls are widely used in the packaging, labeling, food service, and printing industries.

3.How does the polyethylene coating protect against moisture?
The polyethylene coating acts as a barrier, preventing moisture from penetrating the paper and affecting its quality and integrity.

4.Can PE coated paper rolls be recycled?
The recyclability of PE coated paper rolls depends on the specific recycling capabilities of the local recycling facilities. It is important to check with local recycling guidelines.

5.Are PE coated paper rolls safe for food contact?
PE coated paper rolls specifically designed for food applications meet safety regulations and are considered safe for direct food contact.

6.Can PE coated paper rolls be customized or printed on?
Yes, PE coated paper rolls can be customized with printing, including logos, branding, product information, or designs.

7.What are the common sizes and thicknesses available for PE coated paper rolls?
PE coated paper rolls come in various sizes and thicknesses, ranging from small widths suitable for individual portions to larger rolls used for industrial purposes.

8.Can PE coated paper rolls withstand high temperatures?
The polyethylene coating on the paper provides heat-sealing properties and can withstand moderate to high temperatures, making it suitable for heat-sealing applications.

9.How long can PE coated paper rolls typically last?
The lifespan of PE coated paper rolls depends on storage conditions and usage. When stored properly, they can last for an extended period without compromising their quality.