Why Custom Packaging Design Matters More Than Ever for Retail Brands

In today’s competitive retail environment, packaging is more than protection — it’s communication. The right custom packaging design can turn an ordinary product into a memorable brand experience.

Modern consumers pay attention to details — colors, textures, finishes, and sustainability all influence how they perceive a brand. Custom packaging helps retail brands:

  • Strengthen brand identity with consistent visual elements

  • Enhance customer experience through premium and thoughtful design

  • Increase perceived value, making products stand out on crowded shelves

  • Reflect sustainability values with eco-friendly materials and smart structure design

For retail and DTC brands, investing in custom printed packaging boxes, reusable bags, and branded accessories is not just about aesthetics — it’s a strategic move that drives sales and brand loyalty.

At Fulinhan Packaging, we help brands bring their packaging vision to life through tailored design, high-quality materials, and advanced printing technology. Our solutions blend creativity, functionality, and sustainability to ensure your packaging tells your brand’s story — beautifully.


📦 Fulinhan Packaging — Custom OEM & ODM Packaging for Retail and Lifestyle Brands.
✉️ info@fulinhan.com | 📞 +86 18259435129

Why More Overseas Buyers Are Choosing Custom Packaging Suppliers in China

In recent years, China has become the preferred destination for global importers seeking high-quality, customizable, and cost-efficient packaging solutions. From retail boxes to sustainable paper bags, Chinese suppliers are reshaping the global packaging supply chain.

So, what’s driving this shift?

  1. Strong OEM & ODM Capabilities – Chinese factories offer flexible customization options, from design and structure to printing and finishing.

  2. Competitive Pricing – Scalable production capacity and efficient logistics keep costs affordable without compromising quality.

  3. Sustainability Focus – More manufacturers are adopting eco-friendly materials and recyclable packaging to meet global market demands.

  4. One-Stop Solutions – Many suppliers now provide complete packaging services — from concept to shipment — helping overseas buyers save time and resources.

For importers and brand owners, partnering with a reliable Chinese custom packaging supplier means access to innovative materials, fast lead times, and professional export service.

At Fulinhan Packaging, we’re proud to support global clients with tailored, high-quality packaging that enhances brand image and sustainability.


📦 Fulinhan Packaging — Your trusted OEM/ODM packaging partner in China.

✉️ info@fulinhan.com | 🌐 www.fulinhan.com | 📞+86 182 5943 5129

Custom Packaging for Evolving Market Needs Adapting to Change

Why Packaging Design Changes Are Important for Brands

In today’s competitive market, packaging redesign isn’t just about a new look—it’s about staying relevant, boosting sales, and connecting with modern consumer values. From sustainability to smart technology, brands must evolve their packaging to stay ahead.

Old Packaging vs New Packaging: Key Drivers of Change

1. Sustainability and Eco-Friendly Packaging

Consumers demand eco-conscious solutions. Switching from hard-to-recycle plastics to compostable or recyclable materials shows commitment to the environment and boosts customer loyalty.

2. Staying Current with Competitors

Study market shelves, test competitor packaging, and adapt. Learning directly from what works for others ensures your brand stays competitive.

3. Technology and Smart Packaging

Innovations like QR codes, NFC, and active packaging extend shelf life and build deeper customer engagement.

4. Policy & Regulatory Compliance

New industry rules—such as bans on single-use plastics—require timely packaging updates to stay compliant and consumer-friendly.

What Consumers Expect from Modern Packaging

  1. Personalization & Branding: Customized labels and personal touches build stronger connections.

  2. Convenience & Functionality: Easy-to-open, practical designs enhance customer experience.

  3. Authenticity & Storytelling: Packaging that reflects brand values and identity resonates with younger audiences.

How Brands Can Adapt to Evolving Industry Trends

Don’t wait for declining sales—be proactive. A strategic redesign refreshes your brand presence while preserving identity. Gathering outside feedback ensures your packaging resonates with real consumers.

Fulinhan Packaging: Your Partner in New Packaging Design

At Fulinhan Packaging, we help brands navigate packaging transformations—sustainability, design updates, and compliance. Our consultative approach ensures smooth transitions to packaging that is modern, functional, and future-proof.

? Ready to elevate your packaging?
Contact us today for expert design consultation and tailored solutions.


? Email: info@fulinhan.com
? WhatsApp:+86 18259435129
? Website: https://www.fulinhanpackaging.com/

Choosing the Right Nitric Acid Pump for Safe and Reliable Chemical Handling

Choosing the Right Nitric Acid Pump for Safe and Reliable Chemical Handling


Nitric acid is a highly corrosive and volatile chemical widely used in industries such as fertilizers, explosives, and chemical manufacturing. Efficient and safe handling of this aggressive acid requires specialized equipment — particularly a high-quality nitric acid pump. Selecting the right pump ensures not only operational safety but also long-term durability and process efficiency.


Why a Nitric Acid Centrifugal Pump Is Essential

A nitric acid centrifugal pump is specifically designed to handle corrosive liquids under pressure. Unlike general-purpose pumps, these are built with materials that can withstand the oxidizing nature of nitric acid, ensuring a longer service life with minimal maintenance. They provide smooth, continuous flow, making them ideal for large-scale industrial operations where consistent performance is critical.


Chemical Centrifugal Pumps for Aggressive Media

In broader chemical applications, a chemical centrifugal pump is the go-to solution for safely moving aggressive or hazardous fluids. When dealing with acids like nitric acid, pump materials play a critical role. Pumps with metal components often degrade over time, so non-metallic or lined alternatives are necessary to ensure chemical compatibility and maintain safety standards.


Advantages of Teflon-PFA Lined Pumps

For optimal resistance to strong acids, a Teflon-PFA lined pump offers unmatched performance. PFA, a high-performance fluoropolymer, provides excellent corrosion resistance, high-temperature tolerance, and non-stick properties. When used to line a centrifugal pump, it forms a durable barrier between the acid and the pump body, effectively extending the pump's lifespan and reducing risk of leakage.


RISTER PUMPS: Fast Delivery and Proven Nitric Acid Pump Solutions

When it comes to nitric acid handling, RISTER PUMPS has established a strong reputation for delivering reliable, efficient, and safe pump solutions. Their range of nitric acid centrifugal pumps and Teflon-PFA lined pumps are engineered for maximum chemical resistance and operational stability, even under the harshest conditions.

Beyond product quality, one of RISTER PUMPS’ key advantages is speed. With streamlined production and a well-organized supply chain, RISTER offers fast delivery times, ensuring that your projects stay on schedule. Combined with their deep technical expertise and commitment to customer satisfaction, RISTER is the trusted partner for any business requiring high-performance nitric acid pump systems.

Custom Acid Circulating Pumps for Safe and Efficient Chemical Handling

Custom Acid Circulating Pumps for Safe and Efficient Chemical Handling

In industries such as chemical processing, metal finishing, and wastewater treatment, the need for a reliable custom acid circulating pump is essential. Transferring and circulating aggressive acids like sulfuric, phosphoric, and hydrochloric acid requires pumps engineered for corrosion resistance, operational safety, and long service life. Custom-designed pumps offer tailored solutions to meet specific process requirements, ensuring optimal performance under demanding conditions.

Selecting the Right Sulfuric Acid Pump Manufacturer

Working with a reputable sulfuric acid pump manufacturer is key when choosing equipment for harsh acid environments. Sulfuric acid is extremely corrosive, and only pumps made from high-grade materials—such as PTFE, PFA, or other fluoroplastics—can provide the necessary resistance. A good manufacturer will offer custom options in size, capacity, and materials to ensure the pump fits your system perfectly and operates safely over time.

Phosphoric Acid Pump Solutions for Challenging Applications

Phosphoric acid pumps must be specially designed to manage the thick, sticky, and corrosive nature of phosphoric acid. Standard pumps often fail in such conditions due to clogging, corrosion, or material breakdown. Custom acid circulating pumps engineered for phosphoric acid provide smooth, clog-free flow, consistent circulation, and long-term reliability. These pumps are widely used in fertilizer production, food-grade chemical processing, and surface treatment systems.

Magnetic Centrifugal Pumps for Hydrochloride: Safe and Seal-less

For hydrochloric acid applications, a magnetic centrifugal pump for hydrochloride is a smart choice. These pumps use a magnetic coupling to eliminate the need for mechanical seals, one of the most common failure points in acid handling systems. This design minimizes the risk of leaks and exposure, significantly improving plant safety. The combination of magnetic drive technology with acid-resistant materials makes these pumps ideal for continuous circulation of HCl and other volatile acids.

Why RISTER PUMPS Leads in Custom Acid Pump Solutions

As a professional manufacturer of acid pumps, RISTER PUMPS has built a strong reputation for delivering custom-designed solutions that combine performance, safety, and durability. Whether you need a phosphoric acid pump, a magnetic centrifugal pump for hydrochloride, or a tailored solution from a top sulfuric acid pump manufacturer, RISTER delivers pumps engineered for the most aggressive chemical environments.

In addition to product quality, RISTER PUMPS offers significant sales advantages—competitive pricing, fast response times, and flexible order support, even for customized configurations. With global distribution capabilities and technical consultation from experienced engineers, RISTER ensures a seamless buying experience from inquiry to installation. For businesses seeking reliability and performance in acid circulation, RISTER is the name you can trust.

Efficient and Reliable Nitric Acid Pump Solutions for Industrial Applications

Efficient and Reliable Nitric Acid Pump Solutions for Industrial Applications

Nitric acid pump

In the chemical industry, handling highly corrosive liquids like nitric acid requires specialized pumping solutions. A well-designed Nitric acid transfer pump ensures safe, efficient, and leak-free transport of this aggressive chemical in various production processes. RISTER PUMPS, with decades of expertise, provides advanced solutions tailored to the demanding requirements of nitric acid handling.

As a trusted nitric acid pump factory, RISTER designs pumps with corrosion-resistant materials such as PTFE, PFA, and high-grade alloys. These materials provide superior protection against chemical attack, ensuring long service life and minimal downtime. Additionally, RISTER offers designs optimized for energy efficiency and ease of maintenance, reducing operational costs for industrial users.

Our technology is not limited to nitric acid applications. RISTER also manufactures high-performance solutions like the HCL transfer pump, ensuring the safe handling of other strong acids with equal reliability. This multi-chemical compatibility makes our pumps ideal for integrated chemical plants and diverse production environments.


RISTER PUMPS stands out for its engineering excellence, fast delivery times, and technical support throughout the equipment’s lifecycle. Whether for new installations or system upgrades, we provide industrial clients with customized nitric acid pumping solutions that prioritize safety, efficiency, and durability. With RISTER PUMPS, industries can handle even the most aggressive chemicals with confidence.


Efficient Mortar Pump Solutions for Industrial and Construction Applications

Efficient Mortar Pump Solutions for Industrial and Construction Applications

In heavy-duty industries like construction, mining, and chemical processing, a mortar pump plays a vital role in transferring abrasive, viscous mixtures such as cement slurry, lime, or chemical sludge. These pumps must withstand harsh conditions while delivering continuous, clog-free performance. Whether used for grouting, shotcrete, or slurry transfer, selecting the right mortar pump ensures long-term reliability and operational efficiency.

The Role of Pickling Centrifugal Pumps in Corrosive Slurry Handling

For industries that deal with corrosive slurries—such as metal pickling or acid washing—a pickling centrifugal pump is essential. These pumps are designed to handle high concentrations of acid and particulates, making them ideal for transporting chemically aggressive and abrasive mortar-like mixtures. Their non-metallic construction and corrosion-resistant components ensure safe, long-term use in hostile environments.

Why UHMWPE Pumps Excel in Abrasive Applications

When dealing with highly abrasive slurries or mortar mixes, a UHMWPE pump (Ultra High Molecular Weight Polyethylene) is an excellent solution. These pumps offer exceptional wear resistance, high impact strength, and excellent chemical compatibility. UHMWPE mortar pumps are especially valuable in industries where particles in the fluid would quickly degrade metal components. Their ability to extend service life while minimizing downtime makes them a preferred choice for challenging pumping tasks.

Choosing the Right Slurry Pump Manufacturer

Partnering with a reliable slurry pump manufacturer ensures that your equipment is designed for both durability and performance. A qualified manufacturer will provide pumps that are tailored to your specific slurry characteristics—such as particle size, viscosity, and chemical composition—ensuring maximum efficiency and minimal maintenance. Customization options, material selection, and after-sales support are key factors in long-term operational success.

Why RISTER PUMPS is Your Ideal Mortar Pump Partner

RISTER PUMPS stands out as a trusted provider of mortar, slurry, and chemical transfer pumps, offering a wide range of corrosion- and abrasion-resistant solutions. Whether you need a pickling centrifugal pump, a high-strength UHMWPE pump, or guidance from an experienced slurry pump manufacturer, RISTER delivers with precision. Their pumps are engineered with high-performance materials and backed by expert technical support.

In addition to top-tier products, RISTER offers fast delivery, professional customization services, and strong after-sales support—making them a reliable choice for industries seeking high-quality, long-lasting mortar pump solutions.

Conclusion
Choosing the right mortar pump ensures efficiency, safety, and reduced maintenance in demanding applications. With RISTER PUMPS, you benefit from deep technical knowledge, advanced materials like UHMWPE, and proven reliability in corrosive and abrasive environments.

High-Performance H2SO4 Pumps for Industrial Applications

High-Performance H2SO4 Pumps for Industrial Applications

Handling sulfuric acid (H2SO4) is one of the toughest challenges in the chemical industry. Its highly corrosive and oxidizing nature demands specialized equipment that guarantees safety, durability, and efficiency. A well-designed h2so4 pump ensures smooth transfer of sulfuric acid, minimizing risks of leaks, system failures, and costly downtime. For industries ranging from steel pickling to fertilizer production, investing in the right pump technology is not optional—it is essential.

Why Specialized H2SO4 Pumps Are Necessary

Conventional metallic pumps often fail when exposed to sulfuric acid due to severe corrosion. Over time, this leads to reduced efficiency, high maintenance costs, and potential safety hazards. This is why industries rely on advanced solutions such as the OEM Pickling centrifugal pump, engineered specifically for acid pickling lines, and the OEM Plastic centrifugal pump, which offers corrosion-resistant construction using high-quality engineered plastics. Both pump types provide dependable performance in highly aggressive chemical environments.

Material Considerations for Sulfuric Acid Handling

Choosing the right material is critical when selecting an H2SO4 pump. PTFE, PFA, and other advanced fluoropolymers provide excellent corrosion resistance, while engineered plastics offer additional protection against chemical attack. An OEM Plastic centrifugal pump ensures that even concentrated sulfuric acid can be handled safely, maintaining pump longevity and consistent operational performance.

Applications Across Industries

H2SO4 pumps are essential in many industrial processes:

  • Steel & Metal Processing: The OEM Pickling centrifugal pump is widely used in acid pickling lines to remove oxides and scale.
  • Chemical Manufacturing: For transferring concentrated acids in production lines.
  • Fertilizer Industry: Handling sulfuric acid in phosphate fertilizer production.
  • Water & Wastewater Treatment: pH control and neutralization systems.
  • Environmental Protection: Acid scrubbing, exhaust gas cleaning, and recycling applications.

The Importance of Safety and Reliability

Sulfuric acid is not only corrosive but also highly hazardous. A robust h2so4 pump must guarantee leak-free operation, secure connections, and long service life under demanding conditions. Magnetic drive technology has become a popular solution for these requirements, as it eliminates mechanical seals—the most common point of leakage in traditional pumps.

Introducing the CQB-F MAGNETIC PUMP

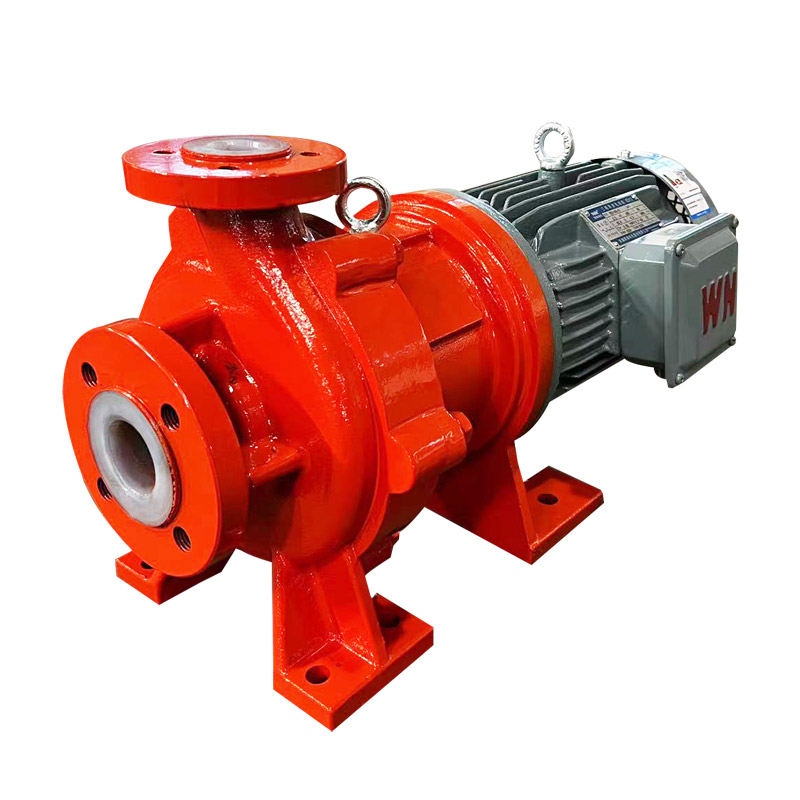
The CQB-F MAGNETIC PUMP is designed specifically for corrosive chemical handling, making it an ideal solution for H2SO4 transfer. Its PTFE-lined construction ensures excellent chemical resistance, while the magnetic drive system provides completely leak-free performance. This pump is suitable for demanding environments such as chemical plants, steel pickling lines, fertilizer facilities, and wastewater treatment systems. It combines efficiency, durability, and safety, reducing downtime and maintenance costs.
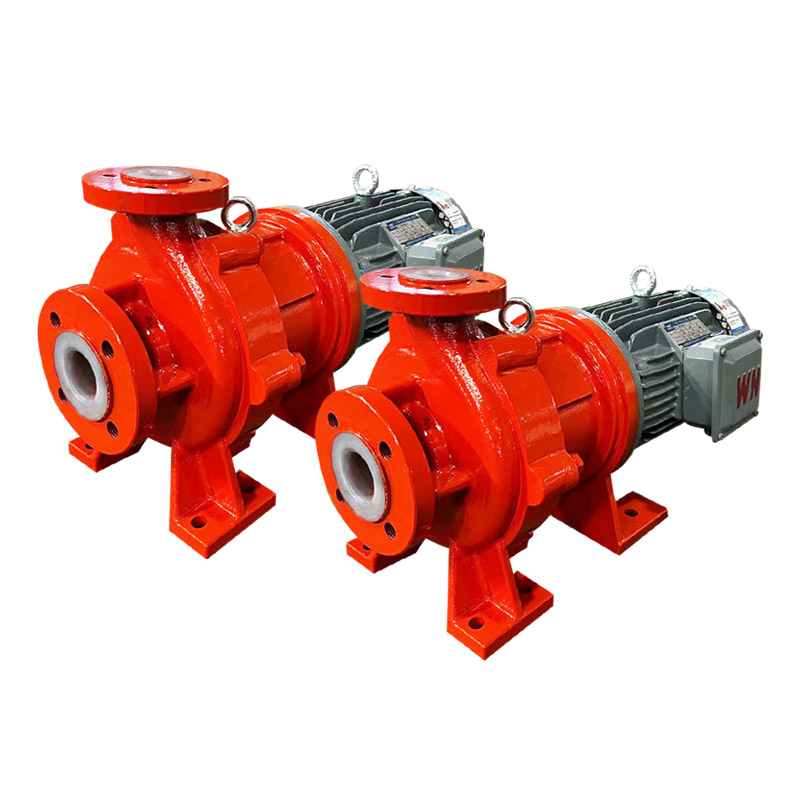
CQB-F magnetic pump

Why RISTER PUMPS Is the Right Choice

Beyond high-quality products, RISTER PUMPS offers comprehensive service advantages that set them apart. From professional technical consultation and customized pump selection to fast delivery and responsive after-sales support, RISTER ensures customers receive complete solutions, not just equipment. With years of expertise in corrosive fluid management, RISTER PUMPS has become a trusted partner for industries requiring reliable and cost-effective H2SO4 pump systems.

Conclusion

Whether for pickling lines, chemical transfer, or environmental protection systems, selecting the right h2so4 pump is critical for safe and efficient operations. With advanced solutions like the OEM Pickling centrifugal pump, the OEM Plastic centrifugal pump, and the cutting-edge CQB-F MAGNETIC PUMP, industries can confidently handle sulfuric acid without compromise. Backed by RISTER PUMPS’ technical expertise and service excellence, clients benefit from reliable, long-lasting, and fully supported pumping solutions tailore
Magnetic Drive Pumps for Reliable Chemical Transfer Applications

Magnetic Drive Pumps for Reliable Chemical Transfer Applications

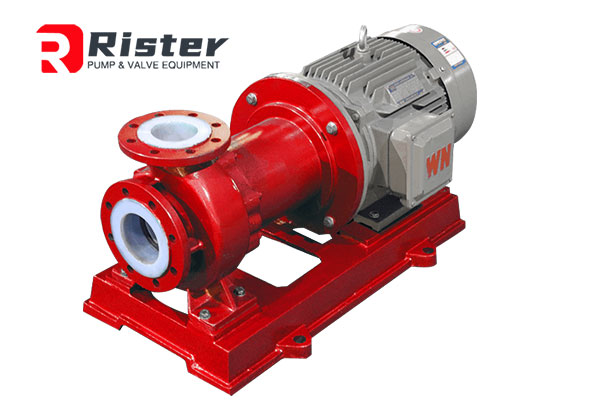
PTFE magnetic pump

In modern chemical processing, selecting the right magnetic drive pump is critical for safe and efficient fluid handling. Unlike conventional sealed pumps, magnetic drive technology eliminates mechanical seals, ensuring leak-free operation when transferring corrosive, toxic, or high-purity liquids. This makes it an ideal solution for demanding applications across the chemical industry.

A high-performance chemical transfer pump must withstand aggressive media such as acids, alkalis, and saline solutions. Magnetic drive designs are widely used as an acid pump and hcl transfer pump, offering excellent corrosion resistance when combined with PTFE, PFA, or other fluoropolymer-lined materials. Their seal-less structure significantly reduces maintenance costs and improves plant safety.

In industries such as water treatment and desalination, magnetic drive pumps are also commonly applied as a brine pump. The smooth internal surfaces and non-metallic wetted parts resist chloride corrosion and scaling, ensuring stable performance in continuous operation environments. Precise flow control further supports efficient chemical dosing and process stability.


With decades of experience in the chemical equipment industry, RISTER provides reliable magnetic drive pump solutions tailored to real industrial needs. RISTER’s engineering expertise, strict quality control, and deep understanding of chemical processes allow customers to achieve long service life, high safety standards, and optimized operating costs. As a trusted partner, RISTER continues to support global chemical plants with proven technology and professional service.

Magnetic Pumps A Leak-Free Solution for Corrosive and Sensitive Fluid Handling

Magnetic Pumps: A Leak-Free Solution for Corrosive and Sensitive Fluid Handling

Magnetic pumps are becoming increasingly popular in industries that demand leak-proof, reliable, and low-maintenance fluid handling solutions. Unlike traditional pumps that rely on mechanical seals, magnetic drive pumps use a sealed design driven by magnetic coupling, which significantly reduces the risk of leakage and contamination. Whether used in chemical processing, water treatment, or marine systems, magnetic pumps offer high efficiency and durability.

Ideal for Salt Water and Corrosive Fluids

One of the key applications for magnetic pumps is handling corrosive media like salt water. A well-designed salt water pump must resist rust and chemical degradation over time. Magnetic pumps, especially those made from corrosion-resistant materials like plastics or Teflon-lined components, are perfect for transferring seawater or brine without suffering internal wear. Their sealed construction prevents moisture intrusion and extends service life, even in harsh coastal or marine environments.

Safe Handling with Hydrochloric Pump Solutions

When transferring strong acids such as hydrochloric acid, equipment safety and compatibility are crucial. A hydrochloric pump must be completely resistant to chemical attack. Magnetic pumps, particularly those lined with PTFE or other chemically inert materials, are ideal for this task. Their seal-less design eliminates the risk of acid leaks, protecting both personnel and surrounding equipment. This makes magnetic pumps a smart investment for chemical plants, laboratories, and acid-handling systems.

RISTER PUMPS: A Trusted Vortex Pump Manufacturer and Magnetic Pump Expert

In the field of industrial pumping, RISTER PUMPS has earned a reputation as a leading vortex pump manufacturer and magnetic pump specialist. Their magnetic drive pumps are engineered for efficiency, safety, and chemical resistance. RISTER offers tailored solutions for a wide range of fluids—from aggressive acids to salt-laden water—ensuring compatibility, durability, and long-term performance.

Beyond product design, RISTER stands out for its strong technical support, fast delivery, and flexible customization services. Whether you're upgrading an existing system or launching a new project, RISTER PUMPS delivers quality and reliability that meet the highest industry standards.

Conclusion

Magnetic pumps are the ideal choice for industries looking to safely handle corrosive or sensitive fluids without the risks associated with mechanical seals. From salt water pumps and hydrochloric pumps to advanced solutions by a trusted vortex pump manufacturer, RISTER PUMPS offers the technology, expertise, and service to support your most demanding fluid transfer applications.