Reliable Magnetic Pump Factory – Precision, Safety, and Chemical Compatibility

Reliable Magnetic Pump Factory – Precision, Safety, and Chemical Compatibility

Excellence in Magnetic Pump Manufacturing

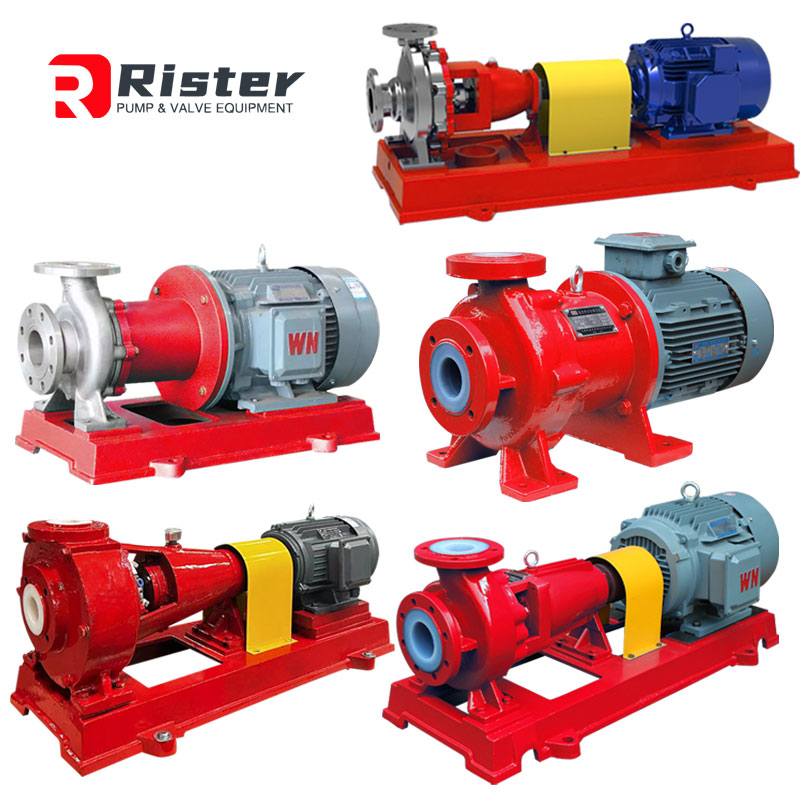
A magnetic pump factory plays a critical role in supporting industries that handle corrosive and hazardous fluids. These pumps are designed with precision to ensure leak-free performance, high efficiency, and chemical compatibility. RISTER PUMPS, as a professional chemical pump manufacturer, has developed a full range of magnetic pumps to serve applications from acid transfer to wastewater treatment, delivering reliability where safety and durability are non-negotiable.

The Importance of Material Selection

Material selection is the foundation of a durable magnetic pump. The teflon pump is one of the most versatile solutions for aggressive chemical transfer. With PTFE or PFA lining, it resists corrosion caused by acids, alkalis, and solvents, ensuring long-term operation even under extreme chemical exposure. This makes it ideal for industries such as chemical processing, electroplating, semiconductor production, and pharmaceuticals.

Magnetic Pumps for Caustic and Acidic Solutions

The caustic soda pump and nitric acid pumps are specifically designed to handle highly reactive and corrosive fluids. Caustic soda, being a strong alkali, requires materials with high resistance to chemical erosion, while nitric acid demands superior corrosion-proof designs. RISTER’s magnetic pumps eliminate traditional sealing problems, ensuring no leakage or contamination, making them perfect for such critical applications.

Energy Efficiency and Maintenance Advantages

One of the key advantages of magnetic pumps lies in their seal-less design. By using a magnetic coupling instead of a mechanical seal, these pumps achieve zero leakage, reduced friction, and longer service life. This design minimizes energy loss, maintenance downtime, and environmental impact—resulting in both cost and safety benefits for industrial users.

Applications Across Multiple Industries

Magnetic pumps from RISTER PUMPS are widely used in diverse industries, including chemical manufacturing, water treatment, pharmaceuticals, metallurgy, and marine applications. Their corrosion-resistant nature allows them to safely handle acids, alkalis, and saltwater in continuous operation environments. From transferring nitric acid in chemical plants to circulating sodium hydroxide in water treatment systems, these pumps perform consistently under challenging conditions.

Quality and Customization from a Professional Magnetic Pump Factory

Every pump produced at RISTER’s magnetic pump factory undergoes stringent quality testing. The company uses advanced production technology, CNC machining, and precision assembly to ensure each unit meets global standards. Additionally, RISTER offers customization for specific process requirements—flow rate, pressure, temperature, and fluid type—providing tailor-made solutions for industrial users.

Environmental and Safety Considerations

Magnetic pumps play a significant role in reducing environmental risk. By ensuring absolute containment of corrosive chemicals, they prevent leaks and accidental spills. This is especially crucial in operations involving hazardous materials like acids or alkalis. RISTER’s engineering team focuses on safety, sustainability, and compliance with international environmental standards.

The Advantage of RISTER as a Chemical Pump Manufacturer

As a trusted chemical pump manufacturer, RISTER PUMPS provides more than just products—they deliver complete fluid handling solutions. Their magnetic pumps are recognized for high chemical resistance, energy efficiency, and low maintenance needs. Beyond manufacturing excellence, RISTER’s strength lies in its after-sales service, rapid response, and technical support for global customers.

Conclusion

Whether it’s a teflon pump for acid transfer, a caustic soda pump for alkali circulation, or nitric acid pumps for chemical processing, RISTER PUMPS stands as a reliable partner for industries demanding quality and performance. With expertise in engineering, manufacturing, and customer support, RISTER continues to lead as a professional magnetic pump factory and a trusted chemical pump manufacturer serving global markets with efficiency, safety, and innovation.
Reliable Methanol Transfer Pump Solutions for Safe Chemical Handling.

Reliable Methanol Transfer Pump Solutions for Safe Chemical Handling

Methanol is a highly flammable and volatile chemical widely used across industries such as pharmaceuticals, biodiesel production, and chemical processing. Efficient and safe transfer of methanol requires carefully engineered equipment to prevent leaks, minimize risks, and ensure long-term reliability. A purpose-built methanol transfer pump is essential to handle this low-viscosity, flammable liquid without compromising on safety or performance.


Why Chemical Centrifugal Pumps Are a Popular Choice

A chemical centrifugal pump is commonly used for methanol transfer due to its ability to handle continuous, high-flow operations. These pumps use rotational energy to move fluids and are ideal for low-viscosity liquids like methanol. However, it’s important that the internal materials of the pump are compatible with alcohol-based chemicals to prevent wear, leakage, and fire hazards. RISTER PUMPS offers centrifugal pumps specifically designed with methanol compatibility in mind, ensuring both safety and reliability.


Stainless Steel Magnetic Pumps: A Leak-Free, Explosion-Proof Option

For flammable and hazardous liquids like methanol, a stainless steel magnetic pump offers an advanced solution. Its seal-less design, powered by magnetic coupling, eliminates the risk of leakage—a critical safety factor when handling flammable substances. Stainless steel construction ensures corrosion resistance and durability while maintaining structural integrity under pressure. RISTER PUMPS provides high-performance magnetic pumps engineered with explosion-proof features, making them ideal for safe methanol transfer in sensitive industrial environments.


RISTER’s Technical Expertise in Chemical Pump Solutions

As a trusted name in industrial fluid handling, RISTER PUMPS specializes in the development and manufacturing of high-performance chemical pumps for demanding applications. With a deep understanding of methanol’s chemical and physical properties, RISTER designs pumps that maximize flow efficiency while maintaining chemical compatibility and operational safety. Whether you require a chemical centrifugal pump or a stainless steel magnetic pump, RISTER provides tailored solutions backed by expert engineering and rapid delivery.


Conclusion

Transferring methanol safely requires the right combination of materials, pump design, and engineering know-how. RISTER PUMPS offers industry-leading methanol transfer pump solutions with a focus on quality, safety, and customization. Their expertise in chemical pumps ensures that your system runs efficiently and securely, even under the most demanding conditions. When safety and performance matter, RISTER PUMPS is the partner you can trust.

Reliable Sodium Hydroxide Pump Solutions for Safe and Efficient Caustic Soda Transfer

Reliable Sodium Hydroxide Pump Solutions for Safe and Efficient Caustic Soda Transfer

Sodium hydroxide pump

A Sodium hydroxide pump is a key piece of equipment in chemical processing, water treatment, pulp & paper, and surface finishing industries, where caustic soda must be transferred safely and continuously. Sodium hydroxide is highly alkaline and corrosive, especially at higher concentrations and temperatures, which places strict requirements on pump materials, sealing methods, and operational reliability.

A professional Caustic soda transfer pump must be designed to resist chemical attack while maintaining stable hydraulic performance. Fluoropolymer-lined solutions are widely adopted for this purpose. In particular, a teflon-pfa lined pump provides excellent resistance to NaOH, preventing corrosion, swelling, and contamination. The smooth lining surface reduces crystallization and scaling, helping to maintain long-term flow efficiency and minimize maintenance.

In demanding industrial environments, a reliable NaOH pump should also focus on safety and leak prevention. Magnetic drive centrifugal pumps eliminate mechanical seals, which are often the weakest point in traditional pumps. This seal-less design significantly reduces leakage risk, improves workplace safety, and lowers operating costs through reduced maintenance and downtime.

The advantages of magnetic drive technology are further proven in applications such as the magnetic centrifugal pump for hydrochloride, where aggressive acids require the same high level of chemical resistance and operational safety. This demonstrates the versatility of magnetic centrifugal pumps across both strong alkaline and acidic media in multi-chemical processing plants.

Beyond product performance, RISTER PUMPS offers strong service advantages that add real value for customers. With deep experience in chemical pump engineering, RISTER provides professional selection guidance, customized material solutions, and fast delivery schedules to meet project timelines.

Combined with responsive after-sales support and global service capability, RISTER PUMPS ensures that each sodium hydroxide pumping system delivers long service life, stable operation, and total reliability—making RISTER a trusted partner for caustic soda and chemical transfer applications worldwide.

Select a correct Acid Transfer Pump for chemical enterprises

Select a correct Acid Transfer Pump for chemical enterprises

Acid transfer pumps are essential components in industries where aggressive chemicals are frequently moved between tanks, reactors, or process lines. Whether transferring hydrochloric acid, sodium hypochlorite, or other corrosive fluids, selecting the right pump ensures both operational safety and system longevity. In this article, we explore key pump types and highlight why RISTER PUMPS is a trusted expert in the chemical equipment industry.

The Importance of Selecting the Right Acid Transfer Pump

An acid transfer pump must be designed to withstand the highly corrosive nature of the fluids it handles. Acidic and oxidizing chemicals can quickly degrade standard materials, leading to leaks, equipment damage, and safety risks. That's why chemical plants and processing facilities require pumps built with high-grade, non-reactive materials that resist corrosion and maintain stability under harsh operating conditions.

Applications for HCL Pump and Hypochlorite Pump Solutions

Two common acids in industrial use are hydrochloric acid (HCl) and sodium hypochlorite. A specialized HCL pump must resist strong,highly corrosive acid environments, while a hypochlorite pump needs to manage oxidizing reactions that can corrode many standard metals. RISTER PUMPS designs and manufactures pumps tailored to each of these challenges, ensuring maximum compatibility and process safety.

Teflon Pumps: The Gold Standard for Corrosive Fluid Transfer

Among the best solutions for acid transfer are Teflon pumps, which feature PTFE or PFA linings. These materials provide exceptional chemical resistance and thermal stability. Teflon-lined pumps prevent contamination and wear, making them ideal for handling a wide range of aggressive chemicals—including HCl, sulfuric acid, and sodium hypochlorite—without compromising performance or durability.

Why RISTER PUMPS Leads in Chemical Equipment Solutions

With years of experience and a strong focus on innovation, RISTER PUMPS has become a respected name in the chemical equipment field. The company’s deep expertise in corrosive fluid transfer and its comprehensive range of acid transfer pumps, including HCL pumps, hypochlorite pumps, and Teflon pumps, make it a preferred partner for industries worldwide.

RISTER not only offers high-performance products but also delivers technical consultation, quick customization, and responsive after-sales service. Whether you're building a new chemical process line or upgrading your current system, RISTER’s solutions ensure safety, efficiency, and long-term reliability.

Conclusion

For any operation involving corrosive chemicals, choosing the right acid transfer pump is vital. With advanced materials like Teflon and dedicated product lines for acids like HCl and hypochlorite, RISTER PUMPS combines engineering excellence with industry expertise—delivering solutions that keep your systems safe and productive.

Sewage Centrifugal Pump Solutions for Efficient Wastewater Management

Sewage Centrifugal Pump Solutions for Efficient Wastewater Management

Efficient and reliable wastewater management is essential for industries, municipalities, and treatment plants. A well-designed sewage centrifugal pump plays a key role in transferring wastewater, sludge, and other contaminated liquids safely and effectively. These pumps are engineered to handle solids, abrasive materials, and varying fluid consistencies, making them indispensable for sewage and sludge applications.


Vertical Sewage Pumps for Space-Saving Efficiency

In systems where installation space is limited, a vertical sewage pump offers a practical solution. These pumps are designed to be submerged directly into the fluid, reducing the need for complex piping and saving valuable floor space. RISTER PUMPS provides vertical sewage pumps that ensure stable operation, low maintenance, and high resistance to clogging, making them ideal for both industrial and municipal wastewater systems.


Miniature Magnetic Pumps for Precise, Small-Scale Applications

For smaller or highly specialized fluid transfer applications, the miniature magnetic pump offers precision and chemical resistance in a compact form. Though not typically used for large-scale sewage transfer, these pumps are essential for handling corrosive or delicate fluids in laboratories, small processing units, or dosing systems. RISTER PUMPS manufactures high-quality miniature magnetic pumps with a focus on leak-free, energy-efficient performance.


Horizontal Sludge Pumps for Heavy-Duty Waste Transfer

When dealing with dense, abrasive sludge, a horizontal sludge pump is often the best choice. These pumps are designed to move large volumes of thick fluids containing solids without clogging or excessive wear. RISTER PUMPS’ horizontal sludge pumps are built with durable materials and innovative hydraulic designs to ensure long-lasting, reliable operation even in the toughest sludge transfer environments.


RISTER PUMPS: Manufacturing Excellence in Fluid Transfer Solutions

As a leading manufacturer in the fluid handling industry, RISTER PUMPS offers a complete range of sewage, sludge, and specialty pumps tailored to meet the demands of various industries. From robust sewage centrifugal pumps to precision-engineered miniature magnetic pumps and heavy-duty horizontal sludge pumps, RISTER combines advanced technology, quality materials, and rapid delivery to provide reliable solutions.

With strong R&D capabilities and a commitment to customer service, RISTER PUMPS stands out not only for its superior product line but also for its ability to deliver customized pumping solutions that improve efficiency, safety, and cost-effectiveness in wastewater and industrial applications.

Sodium Hypochlorite Centrifugal Pump Solutions for Safe and Reliable Chemical Handling

Sodium Hypochlorite Centrifugal Pump Solutions for Safe and Reliable Chemical Handling

Sodium hypochlorite, widely used in water treatment, chemical processing, and cleaning industries, is highly corrosive and requires specialized equipment for safe transfer. A sodium hypochlorite centrifugal pump ensures efficient flow, leak-free operation, and long-term durability when handling this aggressive chemical. Selecting the right pump is essential to avoid corrosion, contamination, and premature equipment failure.


Versatility in Chemical Handling

A well-engineered centrifugal pump for sodium hypochlorite is often designed to handle other corrosive fluids as well. For example, a custom acid circulating pump can be adapted for both oxidizing agents like sodium hypochlorite and strong acids such as sulfuric or phosphoric acid. Similarly, facilities that require multi-chemical transfer benefit from pumps that can manage both hypochlorite and caustic media without compromising safety or efficiency.


Expertise in Acid and Alkali Solutions

When dealing with highly corrosive substances, sourcing from a trusted hydrochloric pump factory ensures quality and performance. RISTER PUMPS produces advanced centrifugal pumps lined with PTFE or other fluoropolymers, providing resistance against hydrochloric acid, sodium hypochlorite, and other aggressive fluids. For alkali handling, RISTER also manufactures robust caustic soda transfer pumps, allowing industries to streamline operations with reliable equipment designed for diverse chemical environments.


Why RISTER PUMPS Leads the Industry

With extensive expertise in corrosive fluid handling, RISTER PUMPS specializes in high-performance solutions for challenging applications. Their sodium hypochlorite centrifugal pumps are engineered for maximum chemical resistance, minimal maintenance, and long service life. Beyond product quality, RISTER provides technical consultation, fast delivery, and customized designs to meet specific operational needs.


Conclusion

For industries requiring safe and efficient transfer of sodium hypochlorite and other corrosive chemicals, RISTER PUMPS delivers comprehensive solutions—from custom acid circulating pumps to caustic soda transfer pumps—all backed by the experience and reliability of a professional hydrochloric pump factory. RISTER’s engineering expertise ensures that every pump performs with durability, safety, and efficiency in even the harshest environments.

Technical Guide to Choosing the Right Soda Pump for Safe and Efficient Caustic Transfer

Technical Guide to Choosing the Right Soda Pump for Safe and Efficient Caustic Transfer

Handling caustic soda (sodium hydroxide) in industrial processes requires equipment that offers both chemical resistance and operational safety. A soda pump plays a critical role in the transfer, circulation, and unloading of caustic solutions. Whether used in wastewater treatment, chemical manufacturing, or textile processing, the proper pump selection can significantly improve system performance and safety.

Why Chemical Compatibility Matters in Acid and Caustic Handling

Though often used in similar facilities, caustic soda and acids have very different chemical properties, and using the wrong pump materials can lead to equipment failure. For transferring both corrosive acids and strong bases like caustic soda, industries rely on acid transfer pumps that are made from chemically resistant materials. Among the most trusted solutions are Teflon pumps, known for their excellent compatibility with a wide range of aggressive chemicals.

The Advantage of Teflon Pumps in Soda Transfer

Teflon pumps (PTFE or PFA-lined) are highly recommended for transferring caustic soda due to their exceptional resistance to chemical attack and high temperatures. These non-metallic pumps prevent corrosion, scaling, and chemical degradation even in continuous operation. Unlike metal pumps, Teflon-lined pumps ensure longer service life and reduce maintenance, especially in systems where purity and leak-free performance are essential. They are also ideal for dual chemical environments, handling both acids and alkalis without cross-contamination or damage.

Reliable Performance in Acid Unloading Applications

In operations involving both acid and caustic handling—such as tanker unloading or chemical storage systems—selecting a multi-compatible acid unloading pump is crucial. RISTER's Teflon-lined centrifugal and magnetic drive pumps are engineered for such environments, capable of safely transferring various corrosive fluids, including hydrochloric acid, sulfuric acid, and caustic soda. This versatility reduces the need for multiple pump types and simplifies maintenance and inventory.

RISTER PUMPS: High-Performance Soda Pump Solutions

As a professional manufacturer of chemical transfer equipment, RISTER PUMPS offers a full range of specialized pumps, including soda pumps, acid transfer pumps, and acid unloading pumps. With a strong focus on Teflon-lined technology, RISTER ensures that every pump meets the highest standards of safety, durability, and performance. Each product is thoroughly tested and backed by expert engineering support, giving customers confidence in demanding environments.

In addition to top-tier products, RISTER PUMPS stands out with fast delivery times, flexible customization, and responsive after-sales service. Whether you're operating a caustic soda dosing system or a large-scale chemical transfer plant, RISTER provides pump solutions that are as reliable as they are innovative—designed to keep your processes running safely and efficiently.

Technical Insights into Caustic Soda Transfer Pumps

Technical Insights into Caustic Soda Transfer Pumps

Handling caustic soda (NaOH) safely requires specialized pumping solutions that can withstand its highly alkaline and corrosive nature. A well-designed Caustic soda transfer pump is essential for ensuring operational safety, reducing maintenance costs, and extending system service life.


Technical Requirements for Caustic Soda Applications

Caustic soda is highly reactive with common metals, so pumps must be built with non-metallic materials or advanced linings. Engineering options such as Custom Acid circulating pump systems provide flexibility for industries that require tailored solutions. Materials like PTFE, PFA, and engineered plastics are often selected to achieve maximum chemical resistance and reliability.


Performance and Compatibility Across Chemical Systems

In many chemical plants, the Sodium hypochlorite centrifugal pump is used alongside caustic soda transfer systems due to their similar corrosion challenges. Likewise, the ZMD self-priming pump offers reliable startup and transfer capability without manual priming, making it highly suitable for continuous or batch operations where downtime must be minimized.


Industry Applications

Caustic soda transfer pumps are widely applied in chemical production, pulp and paper, textiles, food processing, and wastewater treatment. These pumps not only provide secure handling of sodium hydroxide but also protect downstream equipment from corrosive damage, ensuring process stability and compliance with safety standards.


Pump Type Comparison for Caustic Soda Handling

Pump Type

Key Advantage

Application Suitability

Caustic soda transfer pump

Optimized for NaOH handling

General industrial transfer, dosing

Custom Acid circulating pump

Tailored material and design options

High-demand chemical process systems

Sodium hypochlorite centrifugal pump

Corrosion resistance to oxidizing agents

Water treatment & chemical blending

ZMD self-priming pump

Easy startup without manual priming

Batch transfer, intermittent operations


Advantages of KJB CENTRIFUGAL PUMP and RISTER PUMPS

KJB CENTRIFUGAL PUMP delivers durable and precise pump solutions specifically engineered for corrosive fluids. Combined with RISTER PUMPS, clients benefit from fast delivery schedules, technical support, and reliable after-sales services. This synergy ensures industries receive high-performance pumps supported by world-class service, making RISTER a trusted partner in chemical handling.

Technical Insights into Sulfuric Acid Pumps Choosing the Right H2SO4 Pump for Industrial Applications

Technical Insights into Sulfuric Acid Pumps: Choosing the Right H2SO4 Pump for Industrial Applications

Sulfuric acid (H₂SO₄) is among the most widely used industrial chemicals, essential in sectors such as fertilizer production, petroleum refining, battery manufacturing, and chemical processing. However, its highly corrosive nature requires specially designed sulphuric acid pumps to ensure safe and efficient handling. In industrial environments where uptime, safety, and long-term reliability are critical, choosing the right H2SO4 pumps is a technical necessity rather than a simple equipment choice.

Key Design Considerations for H2SO4 Pumps

Transferring sulfuric acid requires more than just chemical resistance; it demands robust engineering. H2SO4 pumps must withstand a wide range of concentrations—from dilute solutions to highly concentrated forms—and must do so without degrading, leaking, or introducing contaminants. Proper selection of materials, seals, and internal components is crucial. Pumps made from or lined with chemically inert materials such as PTFE (Teflon) are especially effective, as they resist corrosion and maintain structural integrity under extreme operating conditions.

Teflon Pumps: A Superior Solution for Sulfuric Acid Transfer

PTFE-lined or fully Teflon sulphuric acid pumps offer unmatched chemical resistance and thermal stability. Teflon’s non-reactive surface prevents the acid from attacking the pump’s internal components, dramatically extending service life and reducing maintenance frequency. Additionally, Teflon pumps help maintain fluid purity, which is essential in applications where contamination can impact product quality or downstream processes. Their resistance to both high temperatures and chemical attack makes them ideal for handling aggressive acids like sulfuric acid.

RISTER PUMPS: Excellence in H2SO4 Pump Engineering

When it comes to designing and manufacturing reliable H2SO4 pumps, RISTER PUMPS has positioned itself as a leader in the industry. With years of experience in corrosive fluid handling, RISTER specializes in producing Teflon-lined centrifugal and magnetic pumps optimized for sulfuric acid applications. These pumps are engineered with safety, durability, and performance in mind, ensuring stable operation even under the most demanding chemical conditions.

RISTER’s Competitive Advantage

Beyond product quality, RISTER PUMPS delivers added value through technical consulting, rapid customization, and fast delivery cycles. Their team of engineers works closely with clients to provide pump configurations that meet exact system requirements, whether for large-scale chemical production or precise dosing applications. RISTER’s deep understanding of acid dynamics, combined with premium materials and modern manufacturing, makes them the go-to choice for industrial users in need of high-performance sulphuric acid pumps.

In conclusion, handling sulfuric acid safely and efficiently starts with the right technology. With advanced Teflon pump solutions and unmatched industry expertise, RISTER PUMPS offers a complete answer to your H2SO4 pump needs—ensuring long-term safety, operational efficiency, and cost-effectiveness.

Teflon Lined Steel Pipe The Smart Choice for Corrosive Applications

Teflon Lined Steel Pipe: The Smart Choice for Corrosive Applications

In today’s industrial environment, safe and efficient fluid transport is critical—especially when dealing with corrosive, hazardous, or high-purity materials. That’s where Teflon lined steel pipe systems shine. By combining the structural integrity of carbon or stainless steel with the exceptional chemical resistance of PTFE (commonly known as Teflon), these lined pipes offer superior performance in demanding environments.

PTFE lined piping is designed to handle a wide range of aggressive chemicals, from strong acids to organic solvents. The PTFE lining acts as a barrier that resists corrosion, prevents contamination, and ensures long-lasting durability. Whether it’s in chemical processing, pharmaceuticals, or semiconductor manufacturing, Teflon lined systems reduce downtime and maintenance costs significantly.

An efficient piping system is incomplete without the right fittings. Components like the Teflon lined elbow provide smooth, corrosion-proof directional changes in flow, ensuring consistent performance across the entire pipeline. Likewise, a PTFE lined tee allows for secure branching in the system without compromising chemical resistance or mechanical strength.

One of the key advantages of choosing Teflon lined steel pipe solutions is their adaptability. They can withstand a wide range of temperatures and pressures while maintaining a non-stick, low-friction internal surface—helping to preserve product purity and optimize flow dynamics.

Whether you're building a new processing line or upgrading an existing one, choosing PTFE lined piping components—such as Teflon lined elbows and PTFE lined tees—ensures safety, reliability, and longevity. For a complete, corrosion-resistant piping solution, Teflon-lined steel is the industry standard.